Robots flawlessly repeat mistakes. That won’t happen with our solutions. Find out more about stable processes here!

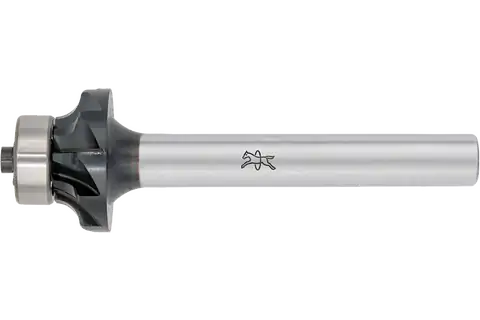
Tungsten carbide burrs for high performance, EDGE, concave radius burrs V EDGE HC-FEP

Tungsten carbide concave radius burr EDGE V14x12mm shank dia. 6mm HICOAT coating defined work on edges, edge rounding radius 2.0mm

V 1412/6 EDGE R2,0 HC-FEP
Item number:
21152930
EAN:
4007220914045
Technical information
Tungsten carbide concave radius burr EDGE V14x12mm shank dia. 6mm HICOAT coating defined work on edges, edge rounding radius 2.0mm

Cut
EDGE HC-FEP
Dia. ball bearing
10 mm
Dia. external
14 mm
Dia. shank
6 mm
Length, construction
12 mm
Length, cut
2 mm
Length, total
52 mm
RPM, grey cast iron, white cast iron
14500 - 23000 RPM
RPM, hard non-ferrous metals
5500 - 7500 RPM
RPM, hardened, heat-treated steels over 1,200 N/mm²
14500 - 19500 RPM
RPM, high-temperature-resistant materials
5500 - 10500 RPM
RPM, soft non-ferrous metals
14500 - 23000 RPM
RPM, steels up to 1,200 N/mm²
14500 - 23000 RPM
Radius corner design
2 mm
Packaging unit
1 piece
Description

Tungsten carbide burrs with the EDGE HC-FEP cut have been especially developed for defined work on edges. The special design allows the burr to run directly along the edges without damaging the workpiece. In just one step, it is possible to achieve precise edge shapes. Among other things, rounding edges is a precautionary measure for anti-corrosion protection according to: ISO 129443, ISO 85013, SOLAS XII/6.3 (Ref. T4/3.01 MSC.1/Circ.1198).

Concave radius burrs for the production of precise radii. Suitable for the production and processing of 2, 2.5 and 3 mm outer radii.

Special features
  • High-quality HICOAT coating for high hardness and wear resistance.
  • Special design for precise guidance.
  • Safe and comfortable to guide.
  • Creates exact edge shapes in one single step.
  • The highly accurate concentricity enables impactfree working without creating chatter marks. This considerably reduces wear on the tool and tool drive.
Recommendations for use
  • Use the burrs counterrotationally. In order to produce a fine surface, finally pass them over the edges in the direction of rotation.
  • If the smallest area of the burr diameter is being used, the recommended rotational speed can be increased accordingly.
Materials that can be worked
Annealed cast iron
Black annealed cast iron (GTS, GJMB)
Brass
Bronze
Case-hardened steels
Cast iron
Cast steel
Cobalt-based alloys
Copper
Grey/nodular cast iron (GG/GJL, GGG/GJS)
Hardened, heat-treated steels over 1.200 N/mm² (< 38 HRC)
Hard non-ferrous metal
Steel
Steel, cast steel
Steels over 700 N/mm² (> 220 HB)
Steels up to 1,200 N/mm² (< 38 HRC)
Steels up to 700 N/mm² (< 220 HB)
Titanium
Titanium alloys
Tool steels
White annealed cast iron (GTW, GJMW)
Zinc
Applications
Chamfering
Deburring
Milling
Rounding
Working on edges
Working on edges (chamfering, rounding)
Drive types
Automated centres
Robot
Straight grinder
Tool machine
Downloads

PFERD TOOLS Newsletter subscription

Register here free of charge for our PFERD TOOLS newsletter and receive all the latest news on products, services and promotions from the world of PFERD TOOLS on a regular basis.